Everything in-house, from design to dispatch.
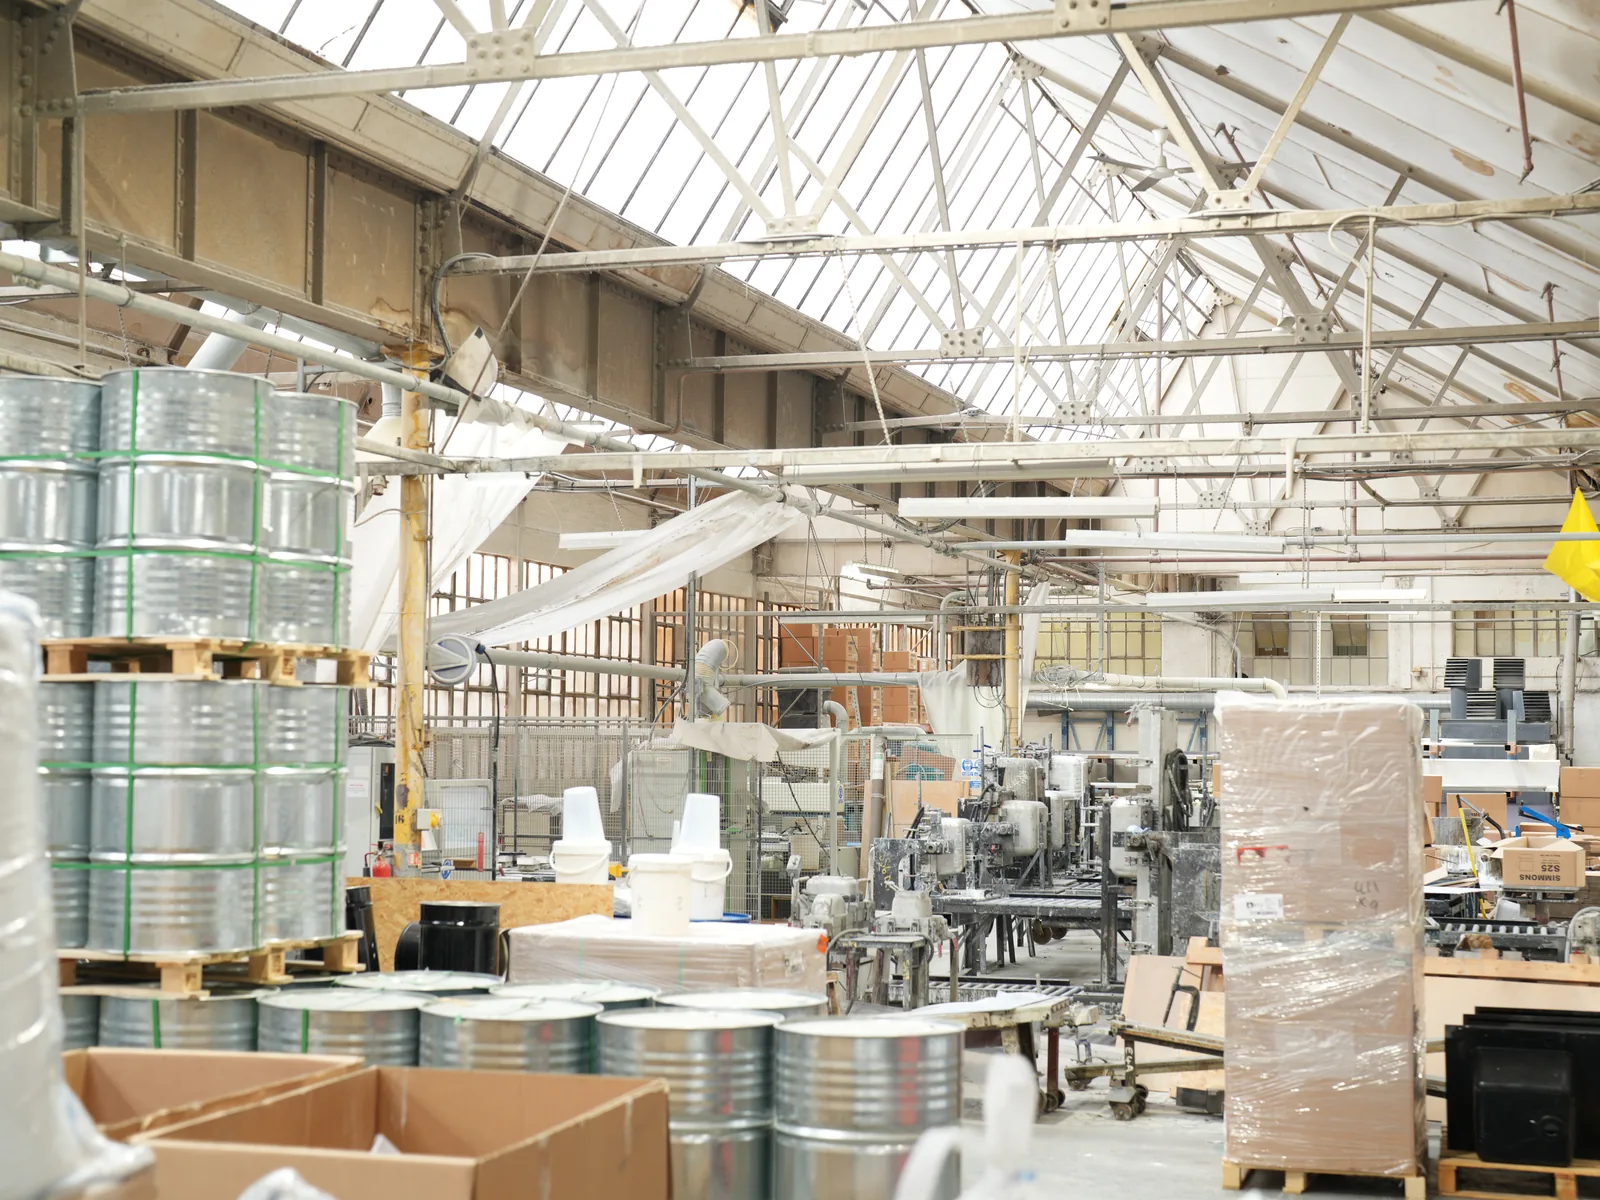
The resin system and every mould are made at Station Street West in Coventry, and so is everything that follows: the castings, the finished tops and the crates they leave in. One site, one material, one team responsible for the whole job.
Simmons worksurfaces are low-pressure cast into cavity moulds, which gives better dimensional accuracy than open-cast sheet, then machined on the 5-axis CNC and fabricated to the customer's specification, in an easy-to-assemble form with the minimum of joints.
Five stages, one site.
The resin, the tooling, the castings, the finished tops and the crates are all made here, so the whole job is held to one specification from the first drawing to the lorry.
- 1
Formulated resin
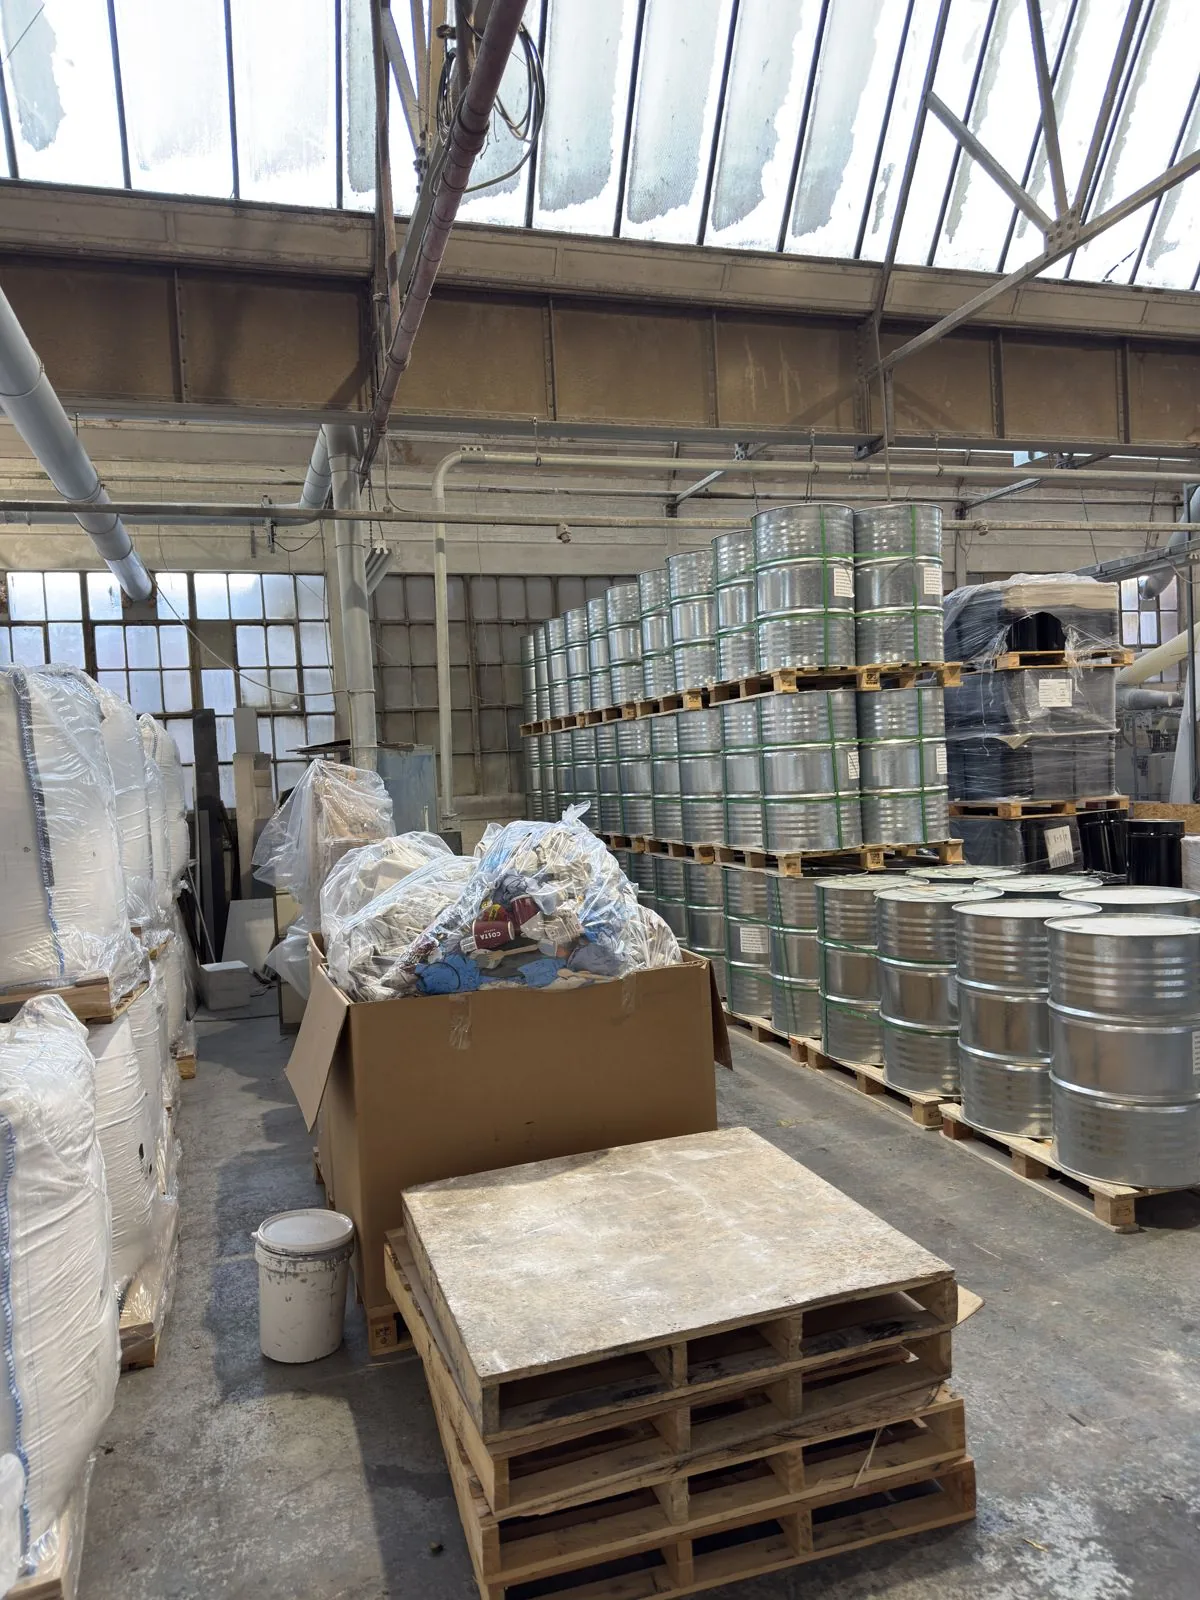
Simmons epoxy is formulated and manufactured in-house for maximum chemical resistance, strength and durability, in five standard colours. Making the resin system here gives Simmons total control over the production process from start to finish.
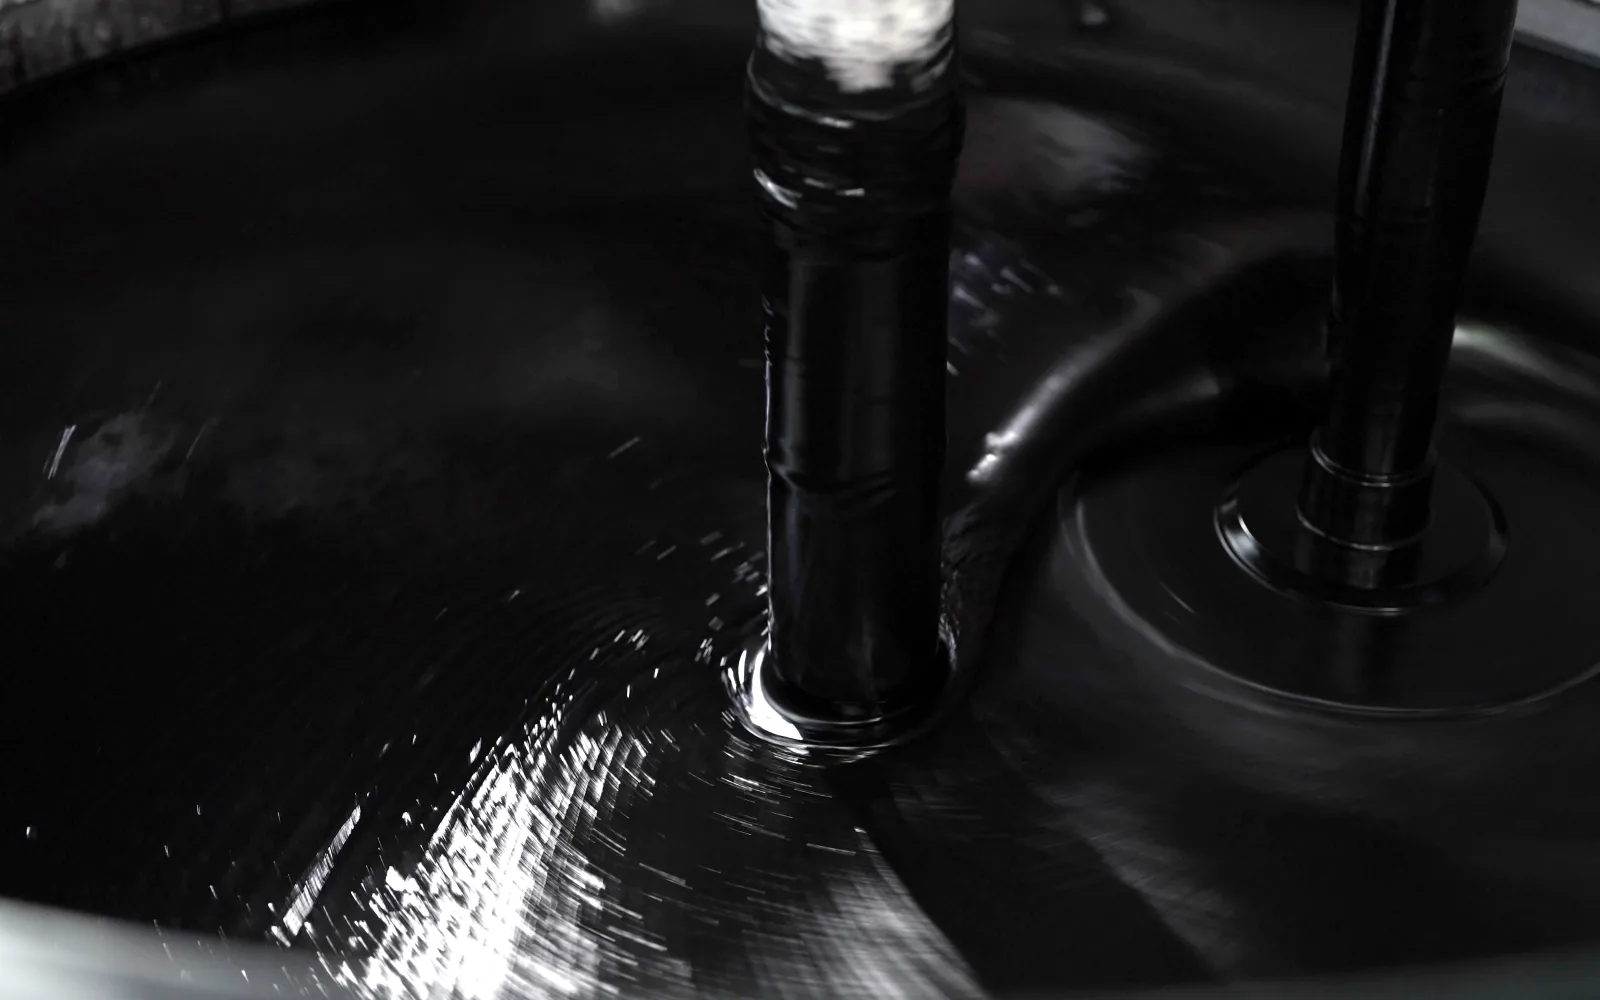
Mixing, Station Street West, Coventry - 2
Moulds and tooling
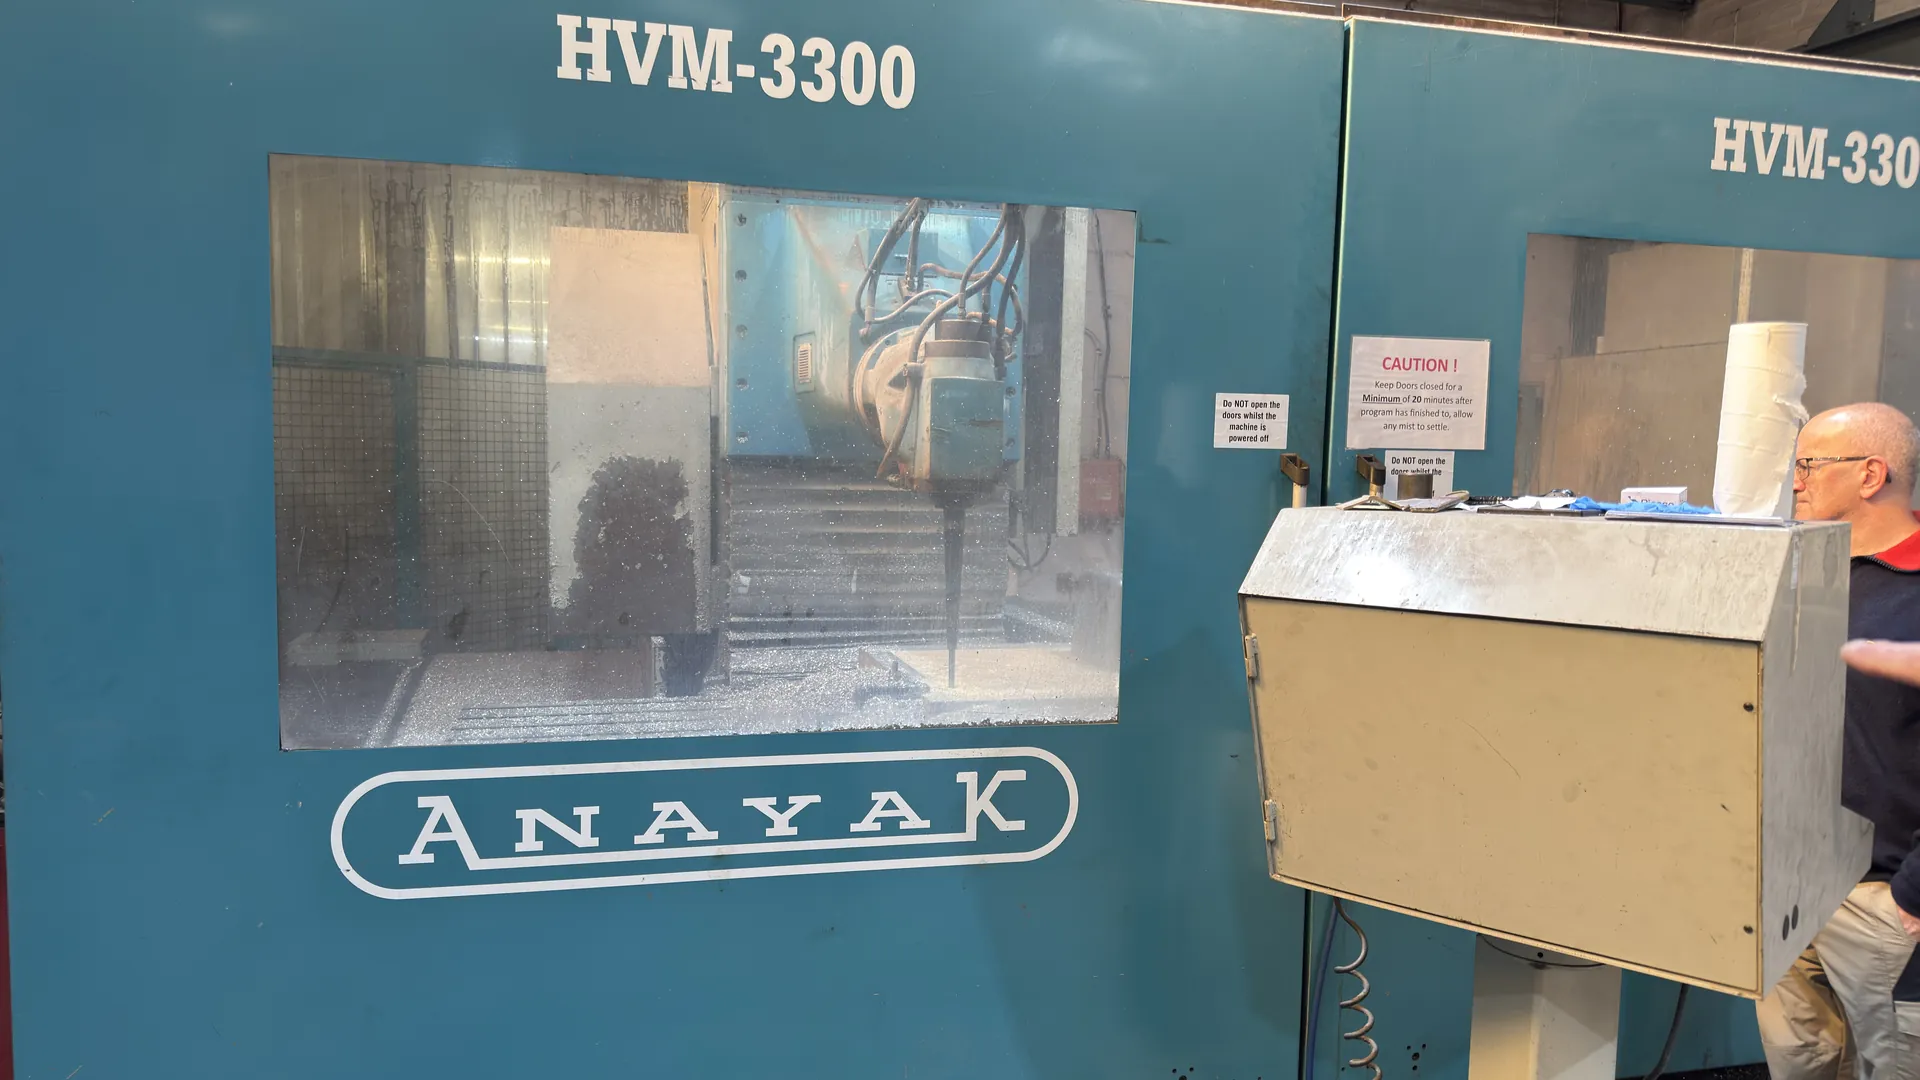
Every mould is made in the tool room at the works. For bespoke work, the new product is designed in solids-based CAD/CAM software, the tooling is made on site on Anayak and Cincinnati three-axis mills, a prototype is cast for the customer to approve, and the mould goes into production. That is why special shapes, drip cups, troughs and non-standard sinks are all possible.
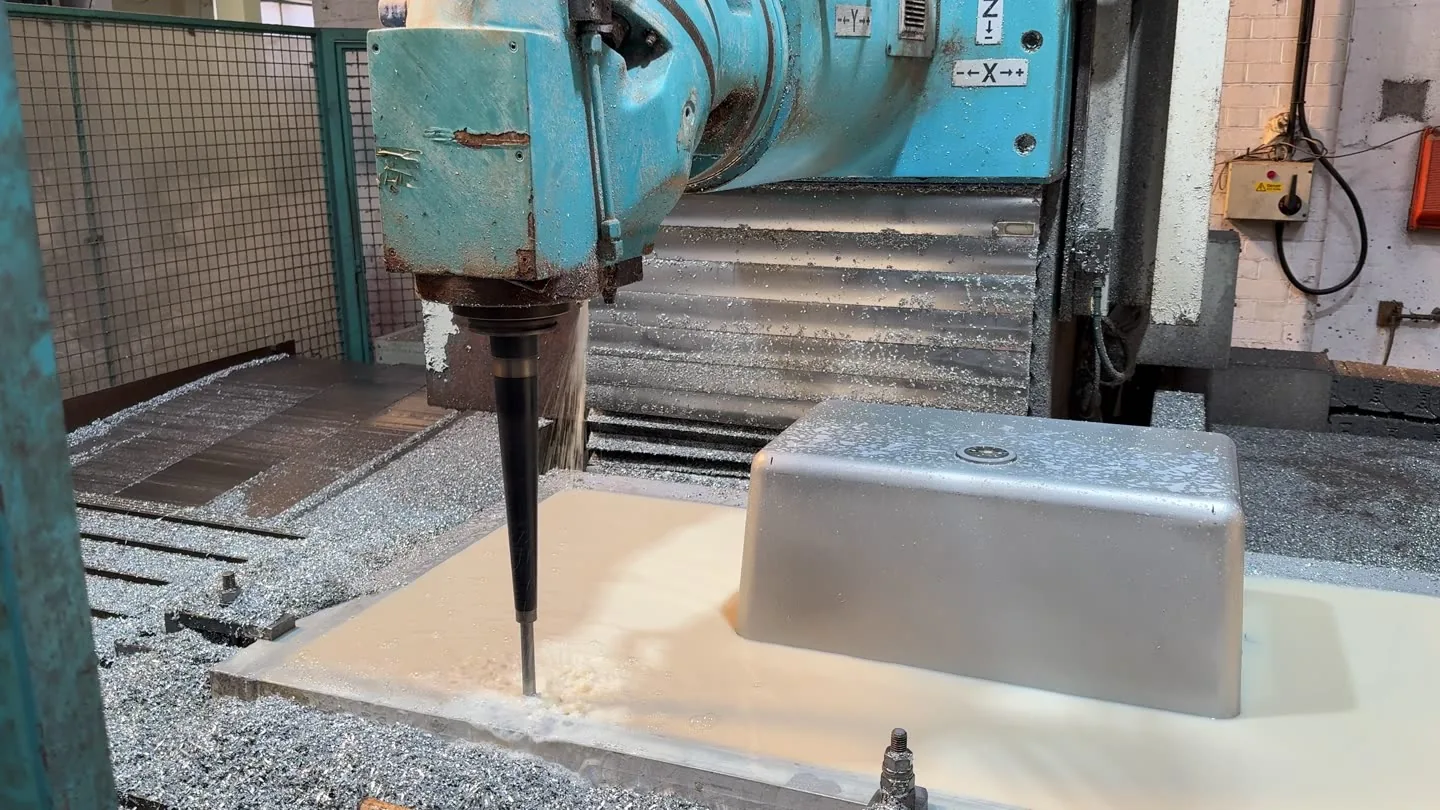
The machining centre, Station Street West, Coventry - 3
Casting
Components are low-pressure cast into cavity moulds, which gives better dimensional accuracy than open-cast sheet. A sinktop or a fume cupboard base comes out of the mould as one seamless casting, with the same material through its full thickness.
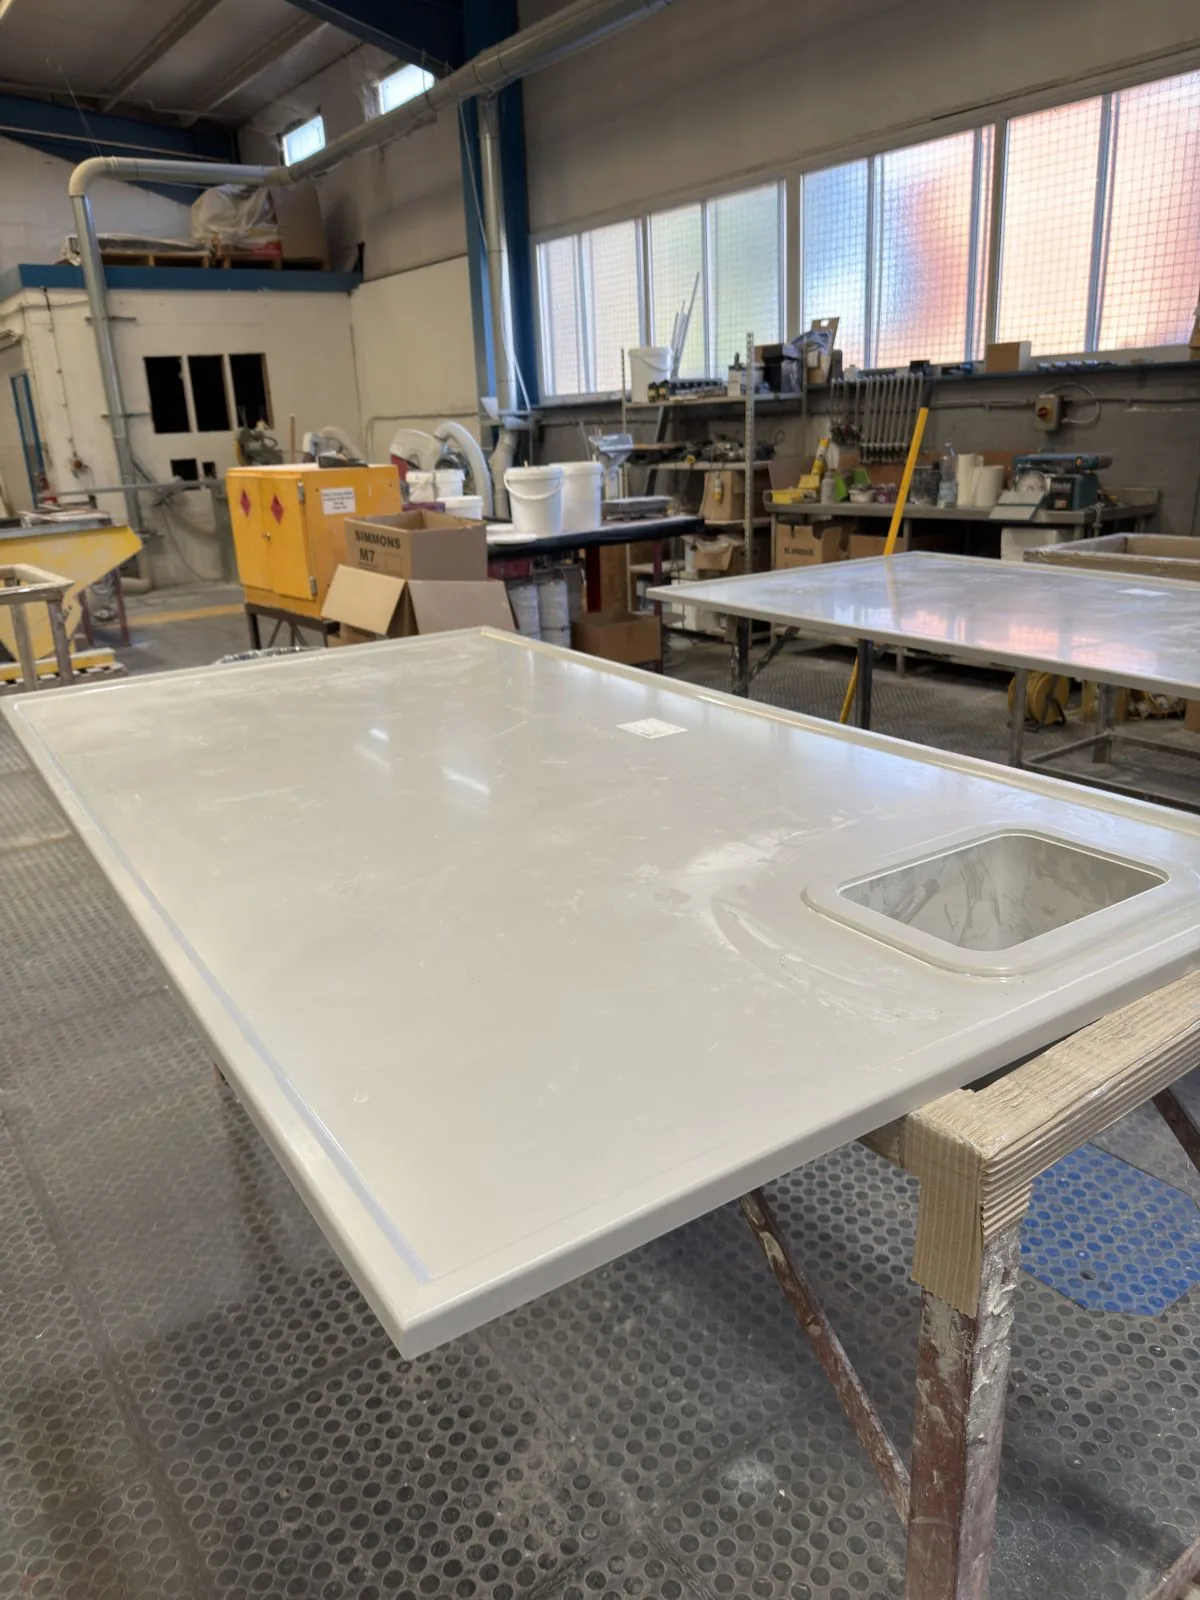
A white casting, Station Street West, Coventry - 4
Machining and fabrication
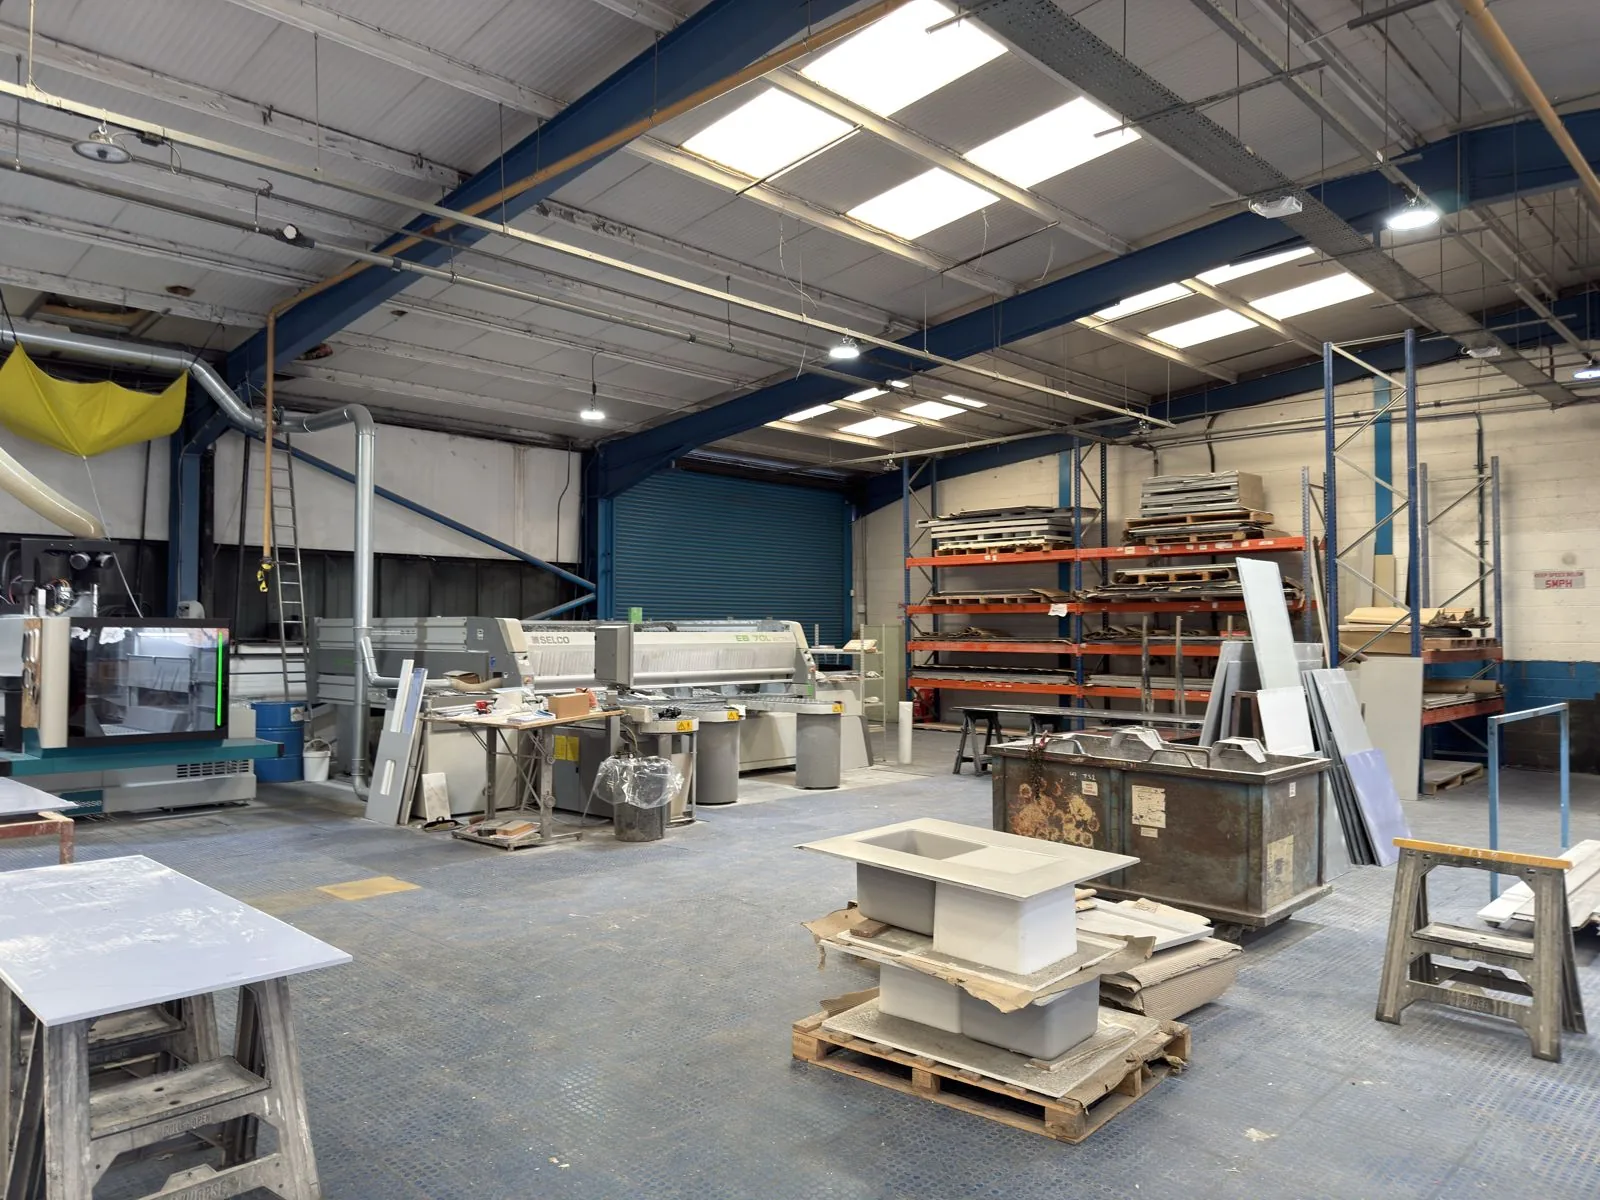
Castings are machined on Biesse five-axis and three-axis machining centres, under a bespoke dust extraction system, components are cut to size on a Selco programmable saw, and tops are fabricated to the customer's drawing. Every assembly is laid out in the works to check dimensional accuracy, the matching of components, the flatness of joints and the overall appearance, so that all items fit together accurately on site.
Watch a sink and worksurface being assembled (22 seconds)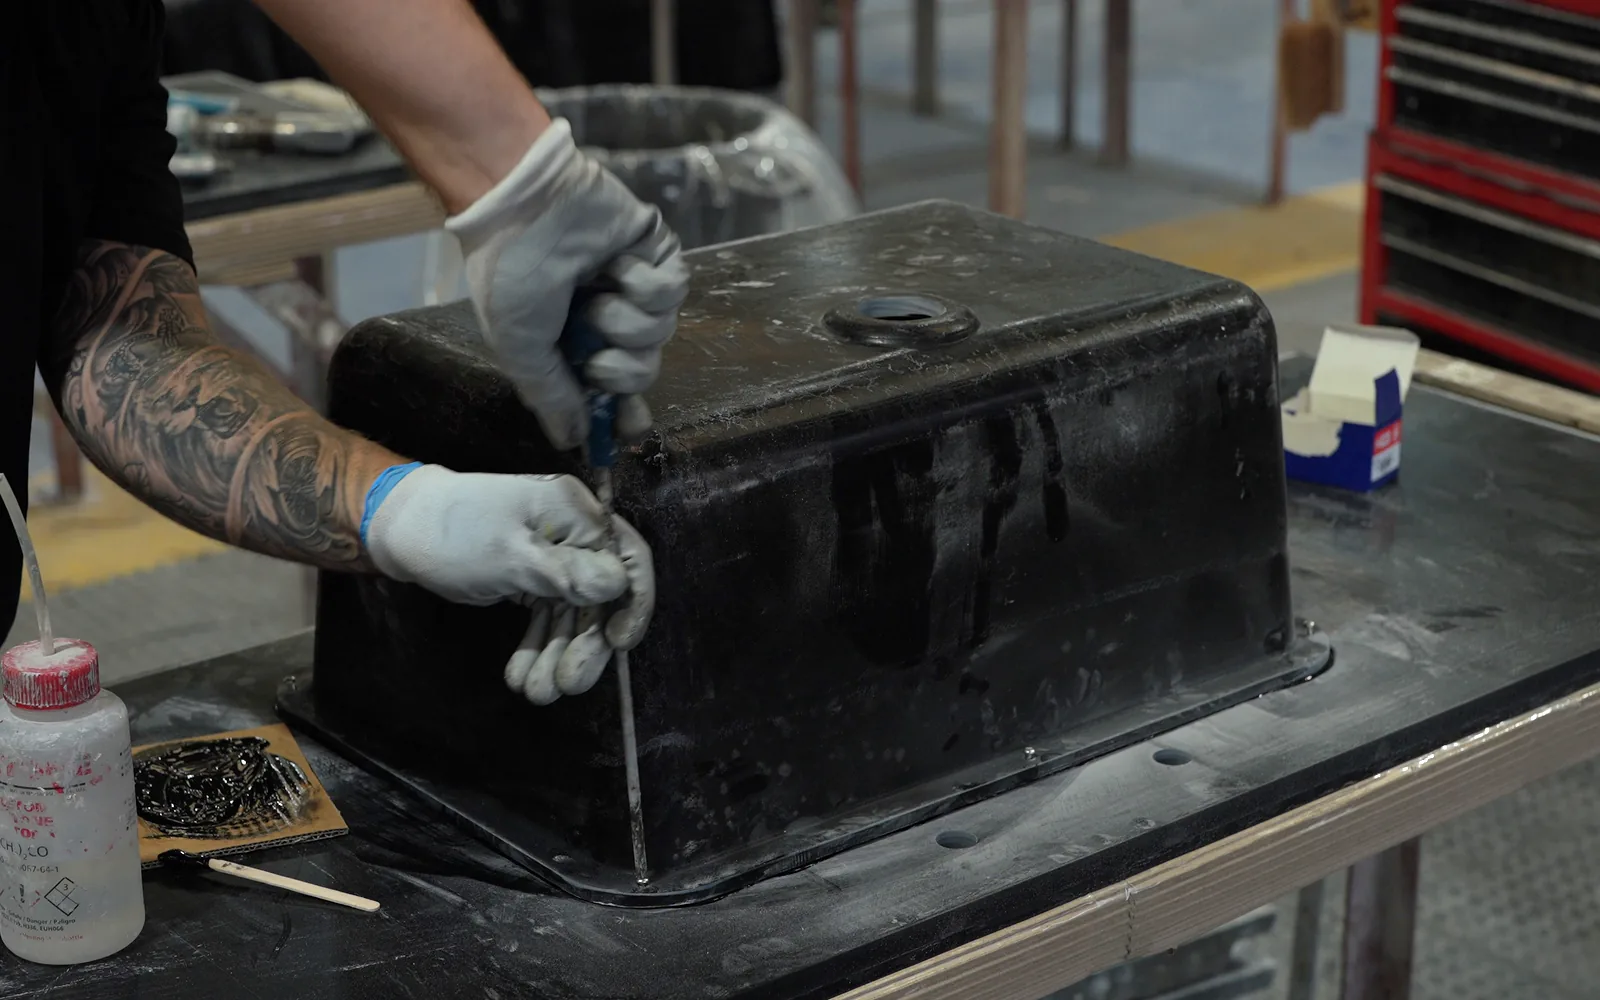
Fabrication, Station Street West, Coventry - 5
Packing and crating
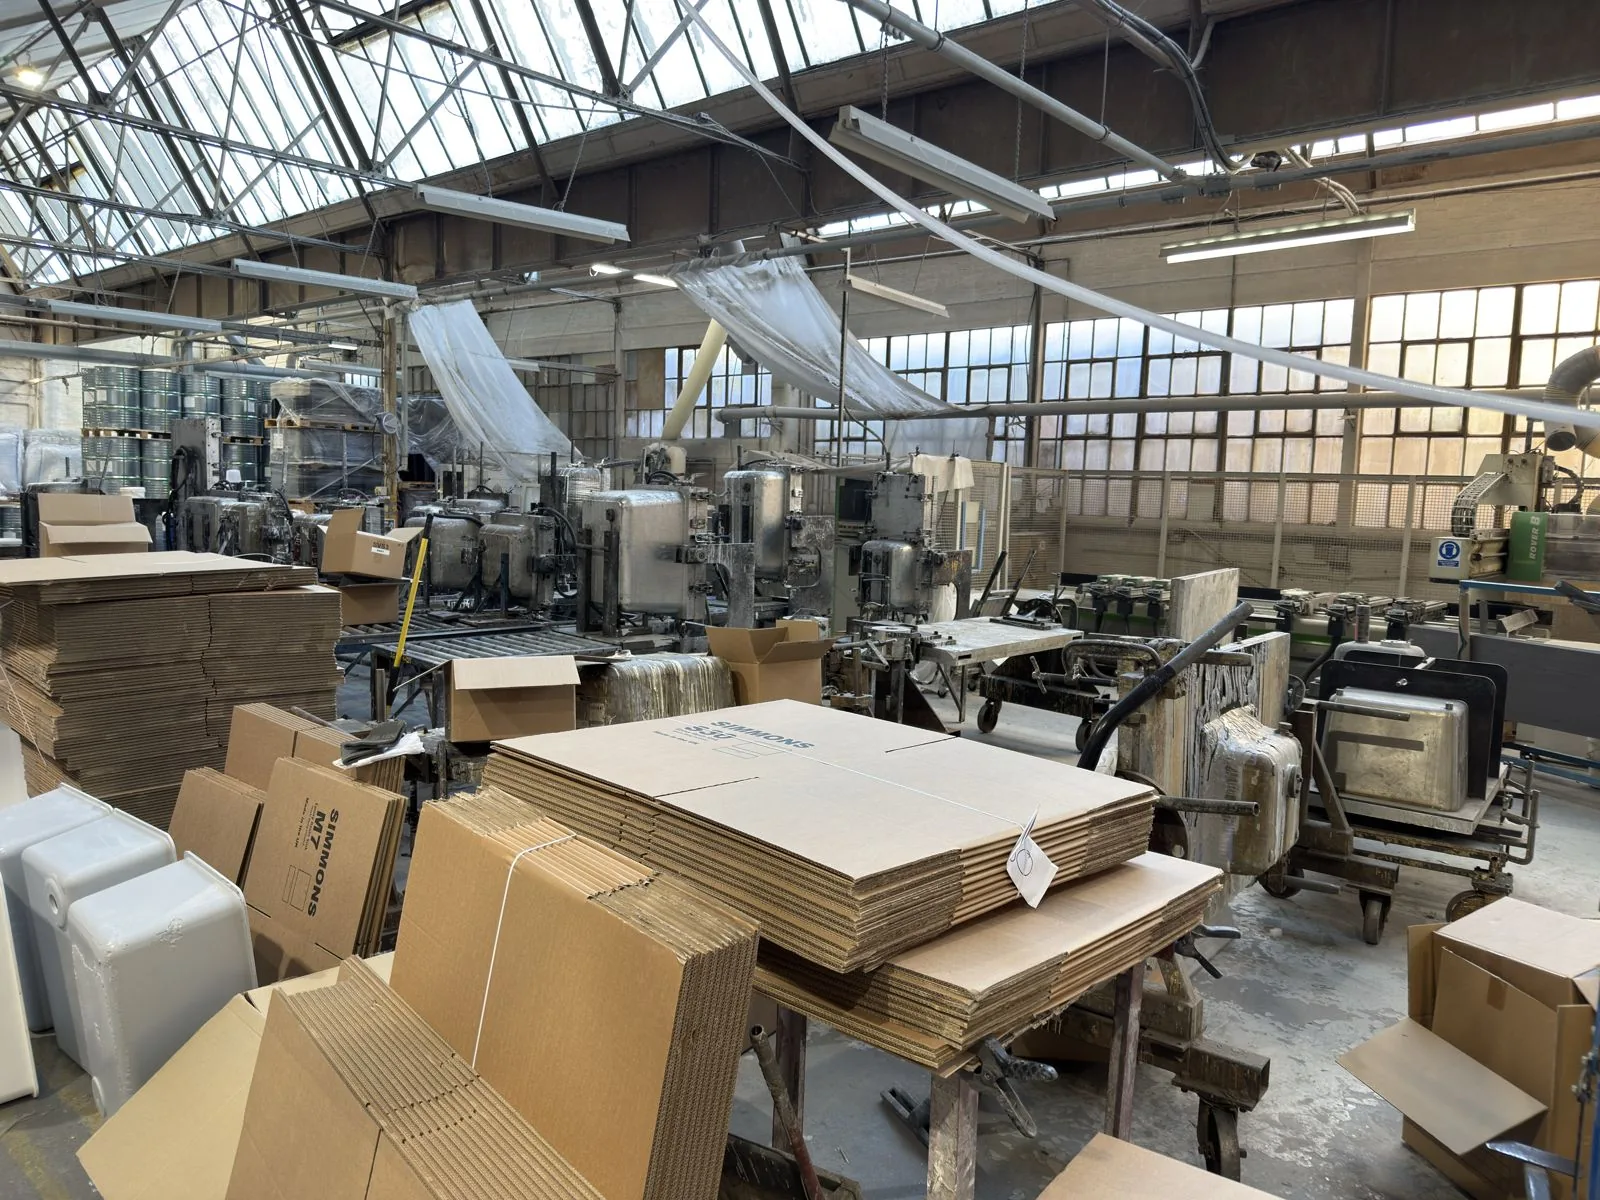
Every consignment is packed at the works. Export crates are built here, to the size of each job, to ISPM 15, the international standard for wood packaging, under UK registration 1210, for shipping to laboratories in more than fifty countries.
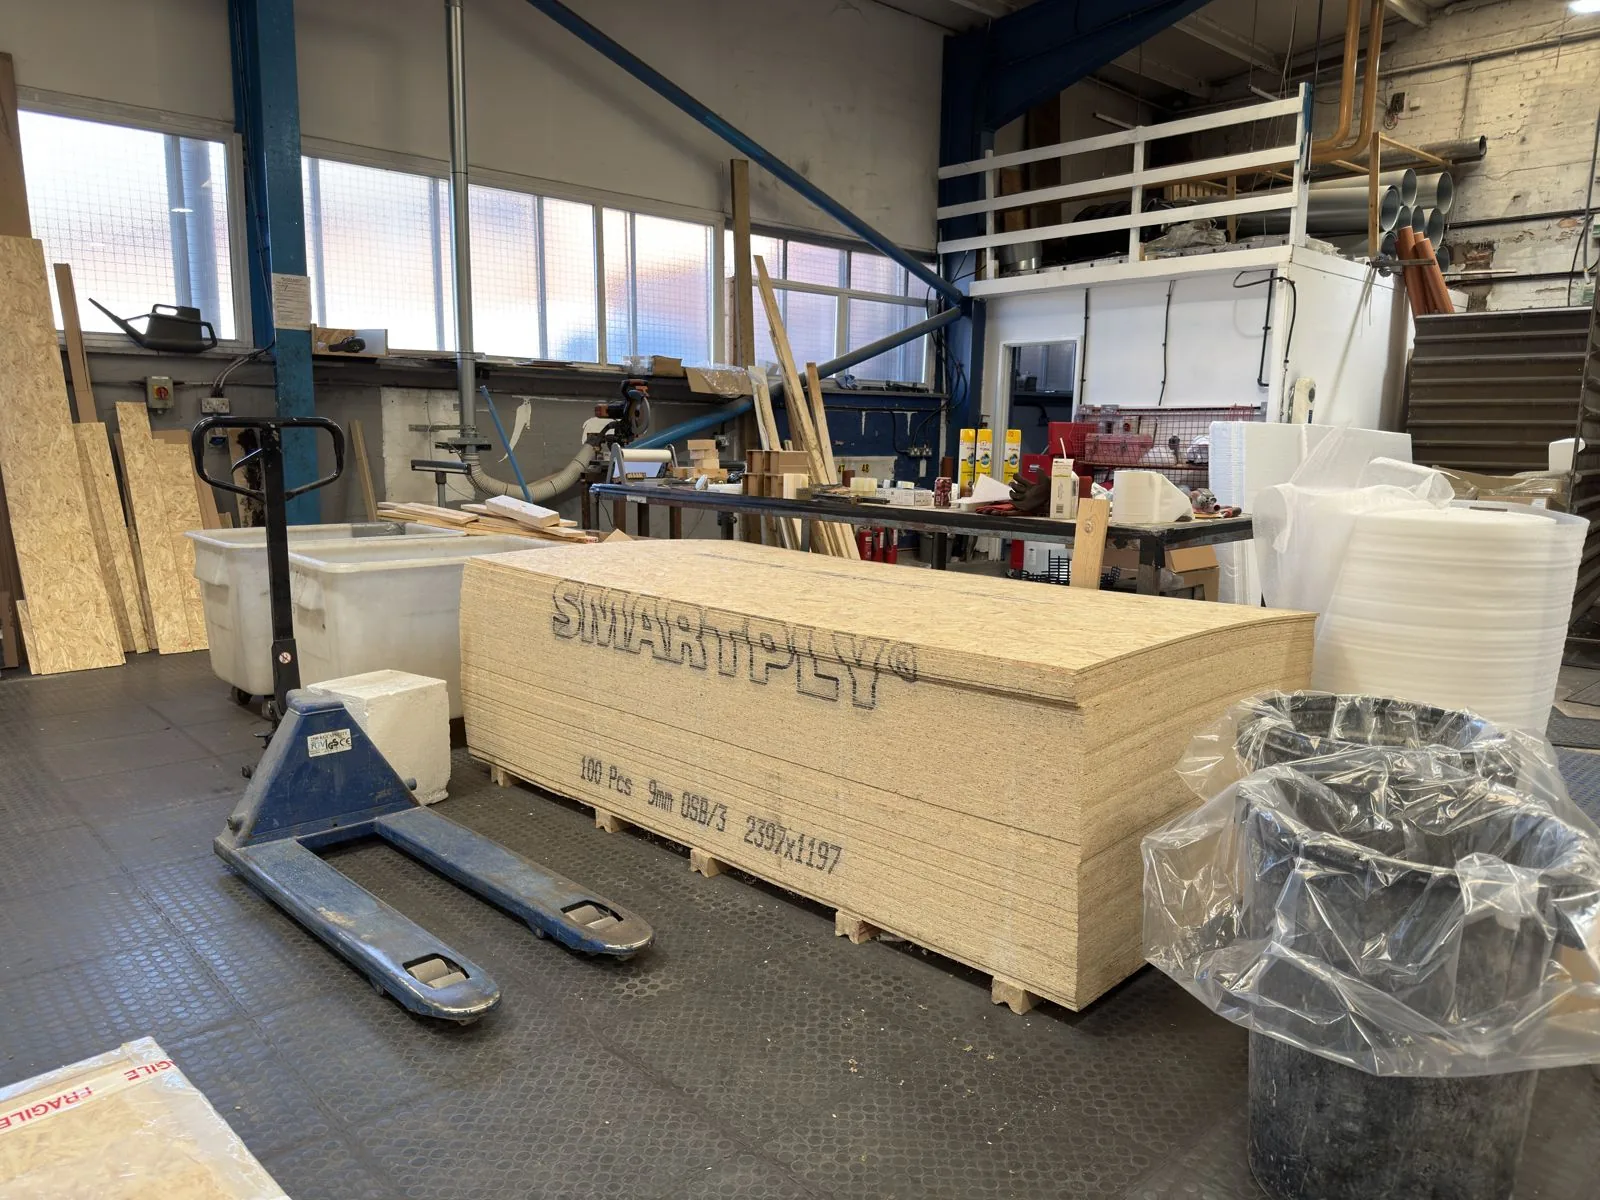
Sheet for export crates, Station Street West, Coventry
Solid through its full thickness.
Components are moulded in a formulated epoxy resin with the same chemical properties throughout their entire thickness. There is no core and no surface layer to wear through or to delaminate; a cut edge is the same material as the top face.
The resin is formulated to allow intricate and complex mouldings: sinks in a range of sizes and fitments, one-piece sink and drainer mouldings, fume cupboard bases and edging strips.
A biscuited joint that meets level.
Where a worksurface needs a joint, Simmons machine a biscuited tongue-and-groove joint so that the top surfaces meet level. Slots are cut along the edges to be joined, accurately located from the top surface; small biscuits are inserted, and the joint is bonded with epoxy resin grout to give a strong, watertight and chemically resistant seal.
Biscuits and grout are supplied with the tops, with full fitting instructions. Joints should be under 1 mm wide: the narrowest joint is always the strongest. How the joint is made on site →
Station Street West, Coventry.
Everything Simmons makes is made here, on one site in Coventry, with the offices on the same ground. The pattern shop and foundry the business grew out of were established in the early 1900s. The story →
- Factory space
- 30,000 sq ft
- Buildings
- Five
- Site
- Four acres
Tell us about your project.
Send your drawings or requirements and our team will come back with a quotation. Need to see the finish first? Request a free sample.